How powder coating protects mild steel enclosures: the 7-tank pretreatment, choosing epoxy or polyester powder, the right thickness, RAL 7035 and IS 5 shade 631, quality tests and common defects.
Powder coating is what stands between a mild steel enclosure and rust. Done well, it lasts for decades; done badly, it peels within a year. This guide explains the process step by step, the pretreatment that matters most, the right thickness and colour, the tests that prove quality and the defects to watch for.
Powder coating is a dry finishing process. A fine powder of resin, pigment and additives is sprayed through an electrostatic gun, which gives the particles a charge so they are attracted to the earthed metal part. The coated part then goes into an oven, typically at around 180–200 °C for 10–20 minutes depending on the powder, where the powder melts, flows and cures into a hard, continuous film.
Compared with liquid paint, powder coating gives a thicker and tougher film in a single coat, has almost no solvent emissions, and overspray can often be recovered and reused. That is why it is the standard finish for electrical enclosures, switchgear panels, control desks and cable trays.
Most powder coating failures — peeling, blistering, rust creeping under the paint — are not caused by the powder. They are caused by poor pretreatment. Steel arrives with oil, rust, mill scale and dust on it; if any of that stays under the coating, adhesion and corrosion resistance suffer.
In India, sheet metal enclosures are commonly pretreated in a multi-tank dip or spray line, often called a 7-tank or 8-tank process:
Galvanised and aluminium parts need a pretreatment designed for those metals; the steel process above is not suitable for them. For the most demanding sites, shot or grit blasting before coating gives the best mechanical key.
| Powder type | Strengths | Limits | Typical use |
|---|---|---|---|
| Epoxy | Excellent adhesion and chemical resistance | Chalks and fades in sunlight | Indoor panels, internal parts, primers |
| Epoxy-polyester (hybrid) | Good finish, economical | Limited UV resistance | Indoor enclosures and panels |
| Polyester (TGIC or TGIC-free) | Good UV and weather resistance | Slightly lower chemical resistance than epoxy | Outdoor enclosures, kiosks, solar boxes |
| Super-durable polyester | Long-term colour and gloss retention | Higher cost | Exposed outdoor and coastal installations |
For an outdoor enclosure, specifying a polyester powder is just as important as the thickness. An indoor hybrid powder used outside will chalk and lose colour within a couple of years.
For electrical enclosures, a dry film thickness (DFT) of about 60–80 microns is a common specification, with thicker systems (for example a zinc-rich or epoxy primer plus a polyester top coat) used for harsh outdoor and coastal sites.
Thickness should be measured at several points on each part with a calibrated magnetic gauge, not just on a flat test panel.
RAL 7035 (light grey) is the most widely used colour for enclosures and control panels worldwide. RAL 7032 (pebble grey) is still seen on older designs. In India, many switchgear specifications call for shade 631 of IS 5, a light grey used for switchgear and panels. Mounting plates are often finished in orange (for example RAL 2000) or left zinc-plated so they stand out from the enclosure body.
Finish can be gloss, semi-gloss, matt or structured (textured). Structured finishes hide minor marks and are popular for control desks and enclosures handled every day.
| Test | What it checks | Common reference |
|---|---|---|
| Dry film thickness | Coating thickness at many points | ISO 2808 |
| Cross-cut adhesion | How well the coating sticks to the metal | ISO 2409 / ASTM D3359 |
| Salt spray | Corrosion resistance over a set number of hours | ISO 9227 / ASTM B117 |
| Impact | Resistance to cracking under a falling weight | ASTM D2794 / ISO 6272 |
| Pencil hardness | Surface hardness and scratch resistance | ISO 15184 / ASTM D3363 |
| Gloss | Consistency of finish | ISO 2813 |
| Cure (solvent rub) | Whether the powder fully cured in the oven | Solvent rub test |
The number of salt spray hours is set by the project specification — there is no single right value — so agree it with the buyer at the start. Salt spray results are useful for comparing coating systems; they do not translate directly into years of service life.
| Defect | What it looks like | Usual cause |
|---|---|---|
| Poor adhesion / peeling | Coating lifts at edges or after impact | Oil or rust left on the steel, weak pretreatment |
| Blistering | Bubbles under the film, often after months outdoors | Salts left from pretreatment, poor rinsing |
| Orange peel | Wavy, dimpled surface | Film too thick, wrong gun settings or cure |
| Pinholes / outgassing | Tiny craters | Gas escaping from welds or porous areas during cure |
| Poor coverage in corners | Thin or bare inside corners | Faraday cage effect — needs gun technique or reduced voltage |
| Colour or gloss variation | Doors and body look different | Different powder batches or uneven cure |
Powder coating is an insulator. Every earth stud, earth bar seat and door earthing point must be masked before coating or cleaned back to bare metal afterwards, otherwise the protective earth connection is not reliable. Threads of welded studs and nuts should also be masked, or the coating will jam the fasteners. Gasket channels need a smooth, even film so the gasket seals evenly and the enclosure keeps its IP rating.
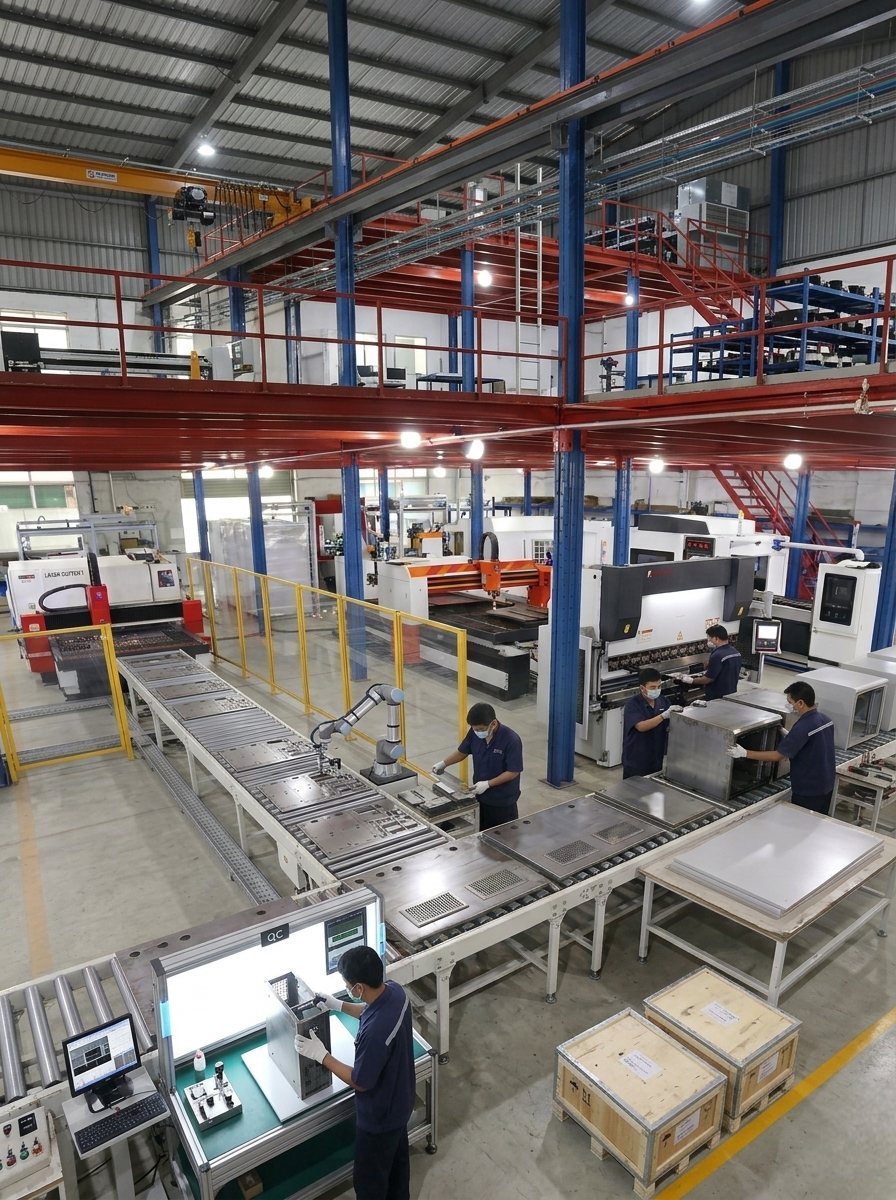
VERCHO Engineering Solutions manufactures powder-coated mild steel enclosures, panels and accessories finished to the colour and specification your project needs. To check whether stainless steel would be a better choice than a coated enclosure, see our guide to choosing enclosure material. For enquiries, write to info@verchogroup.com.
For any question, please write to us at info@verchogroup.com — or send it straight from this page. Our engineering team will reply by email.